Diril is our family name.
It is on every cymbal because every cymbal passes through our hands. This is who makes them, and where.
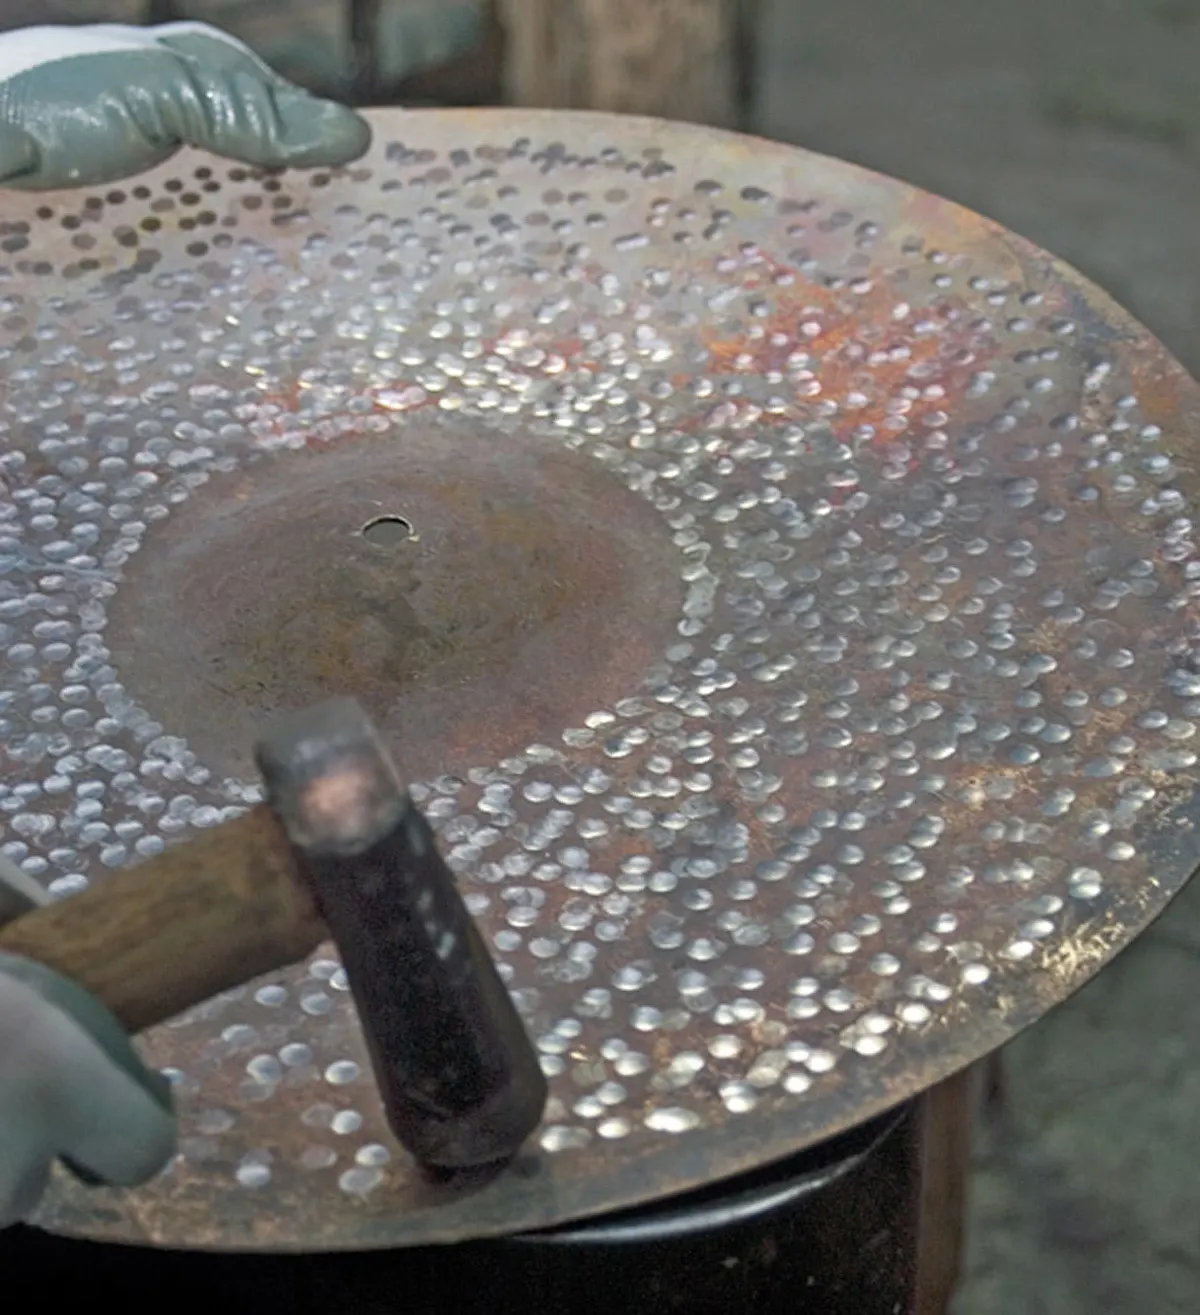
Hammered by hand, so no two Diril cymbals ever sound the same.
Ibrahim Diril, founder
Who we areOld roots. A restless family.
Ibrahim Diril learned to make cymbals in Istanbul, the old way: fire, bronze, a hammer and a good ear. For years the cymbals he hammered went out under other names, Meinl and Paiste among them. In 2008 he put his own name on his work, and Diril was born in Samsun.
Today he works side by side with his four sons in Turkey’s largest cymbal factory. We cast our own B20 bronze, hammer every cymbal by hand and finish it on the lathe, all under one roof. From there, Diril cymbals travel to drummers in more than 50 countries.
Some of the drummers you know already play Diril. Meet them on our Instagram.
Inside the factory.
Fire, hammer and lathe. Every cymbal on this site starts here.
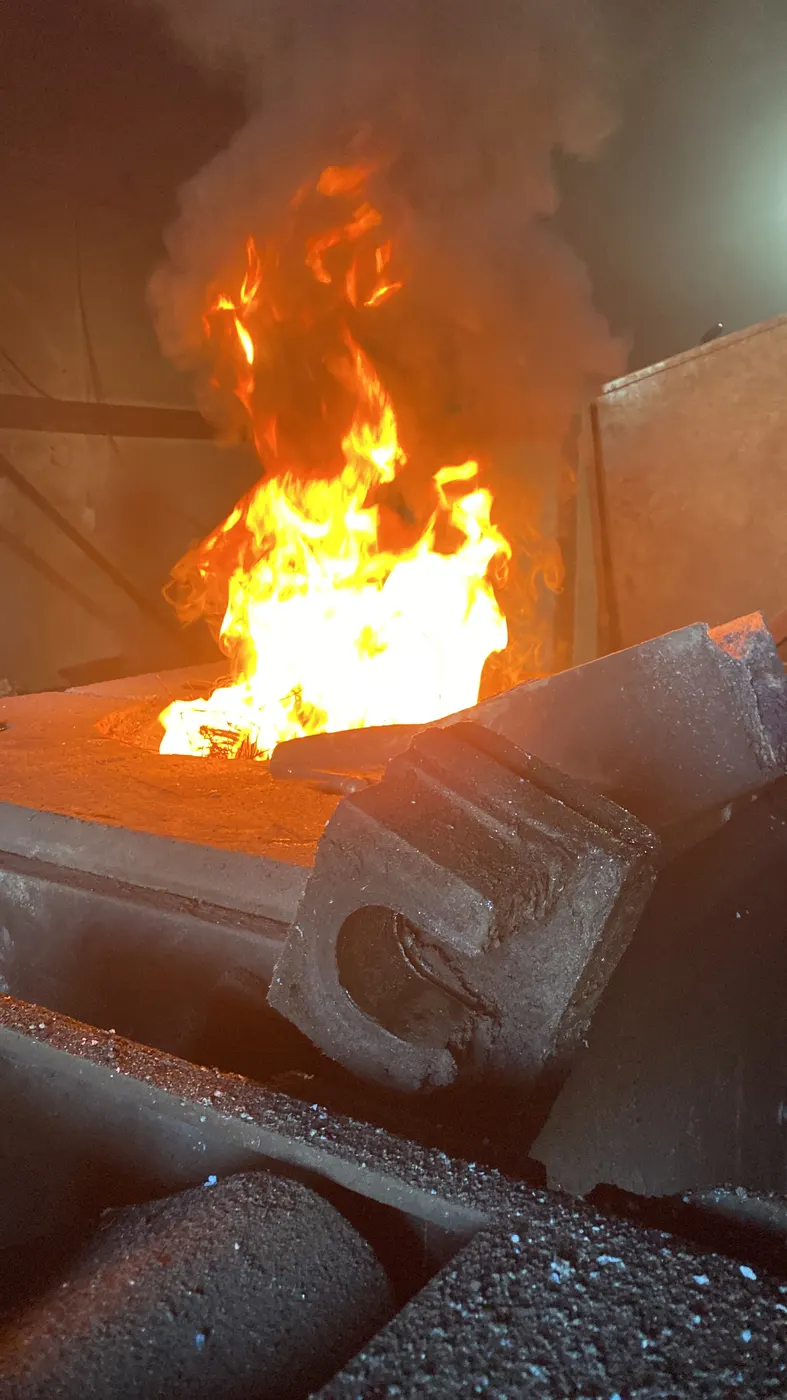
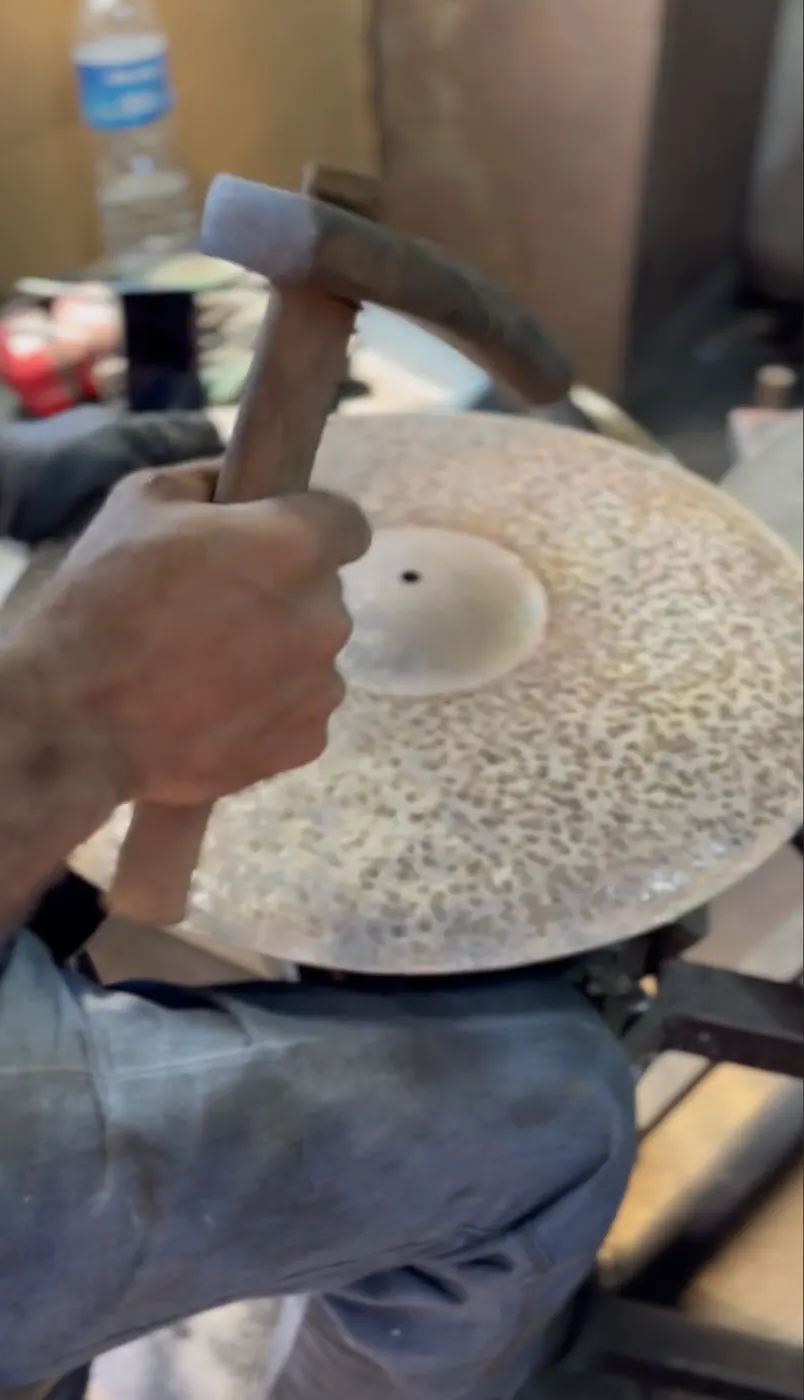
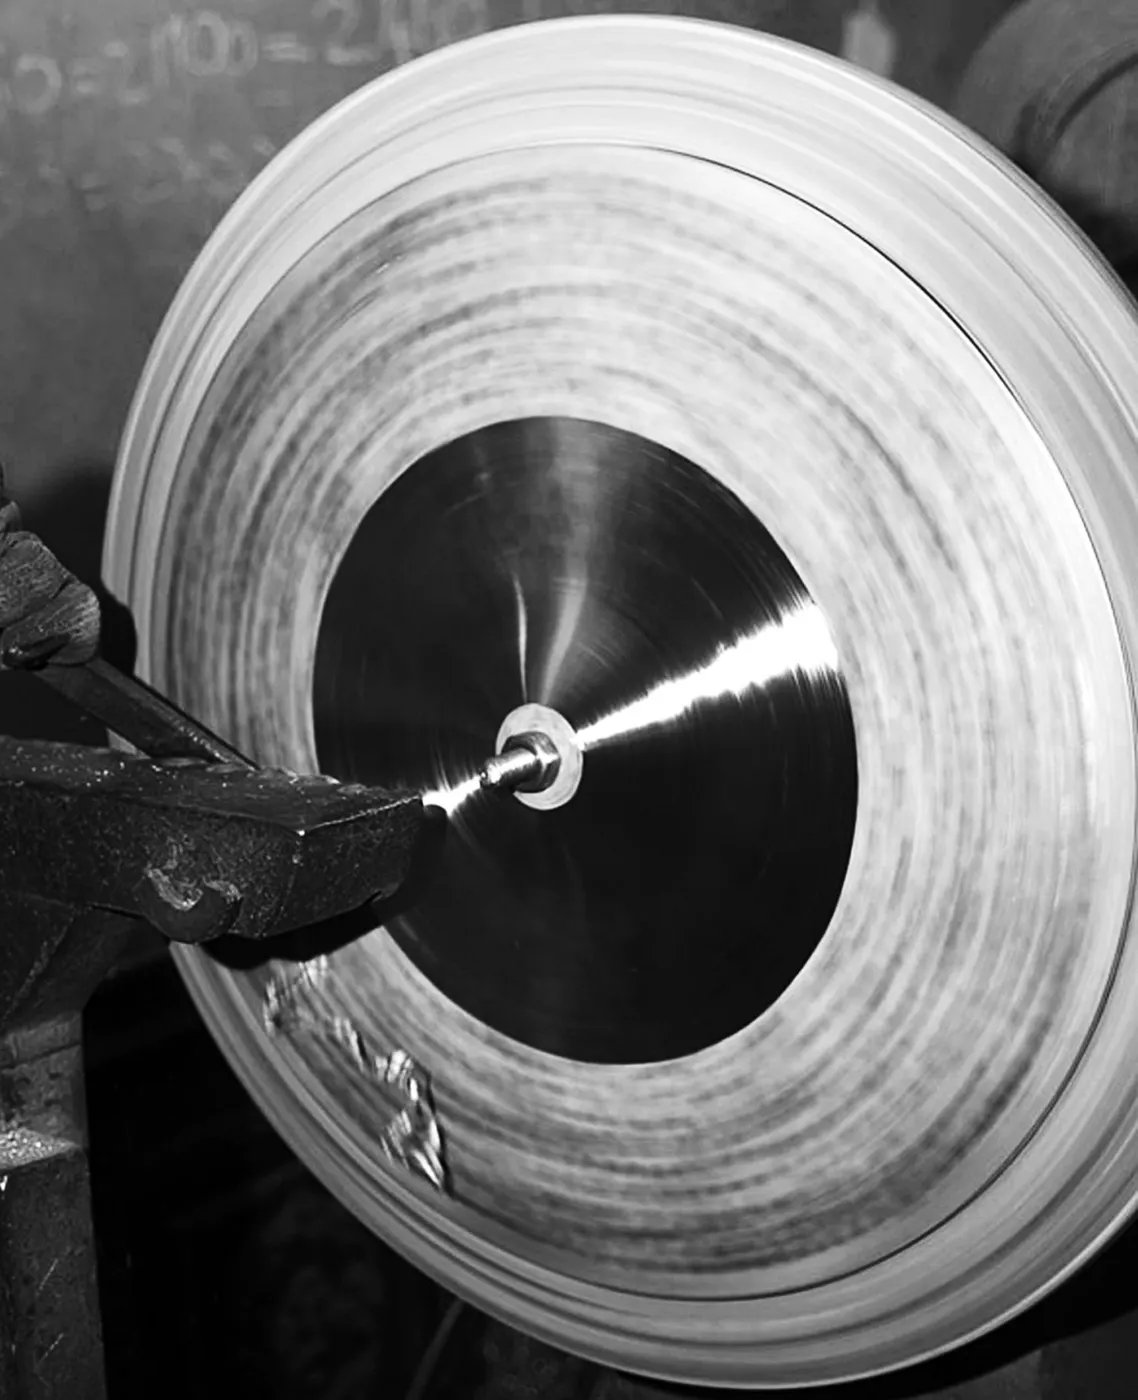
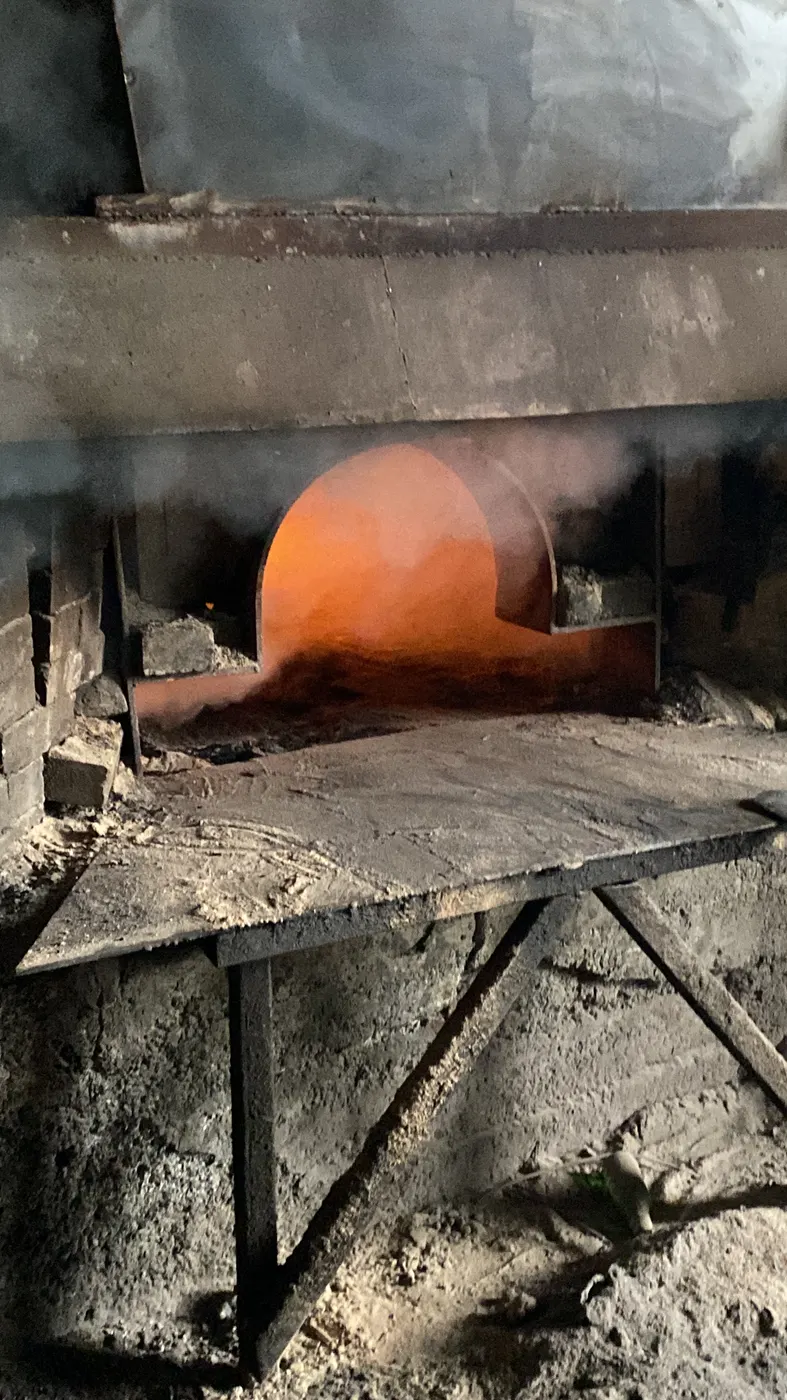
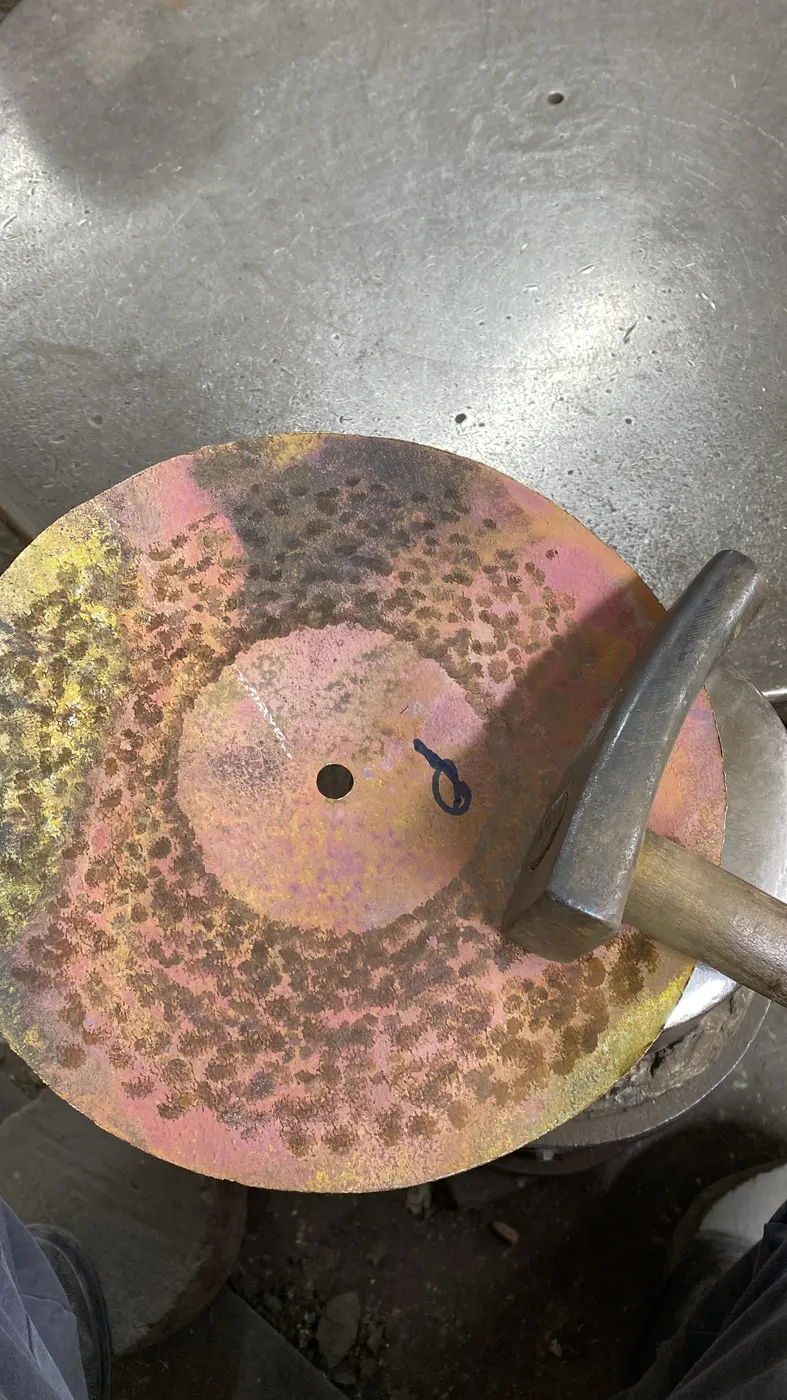
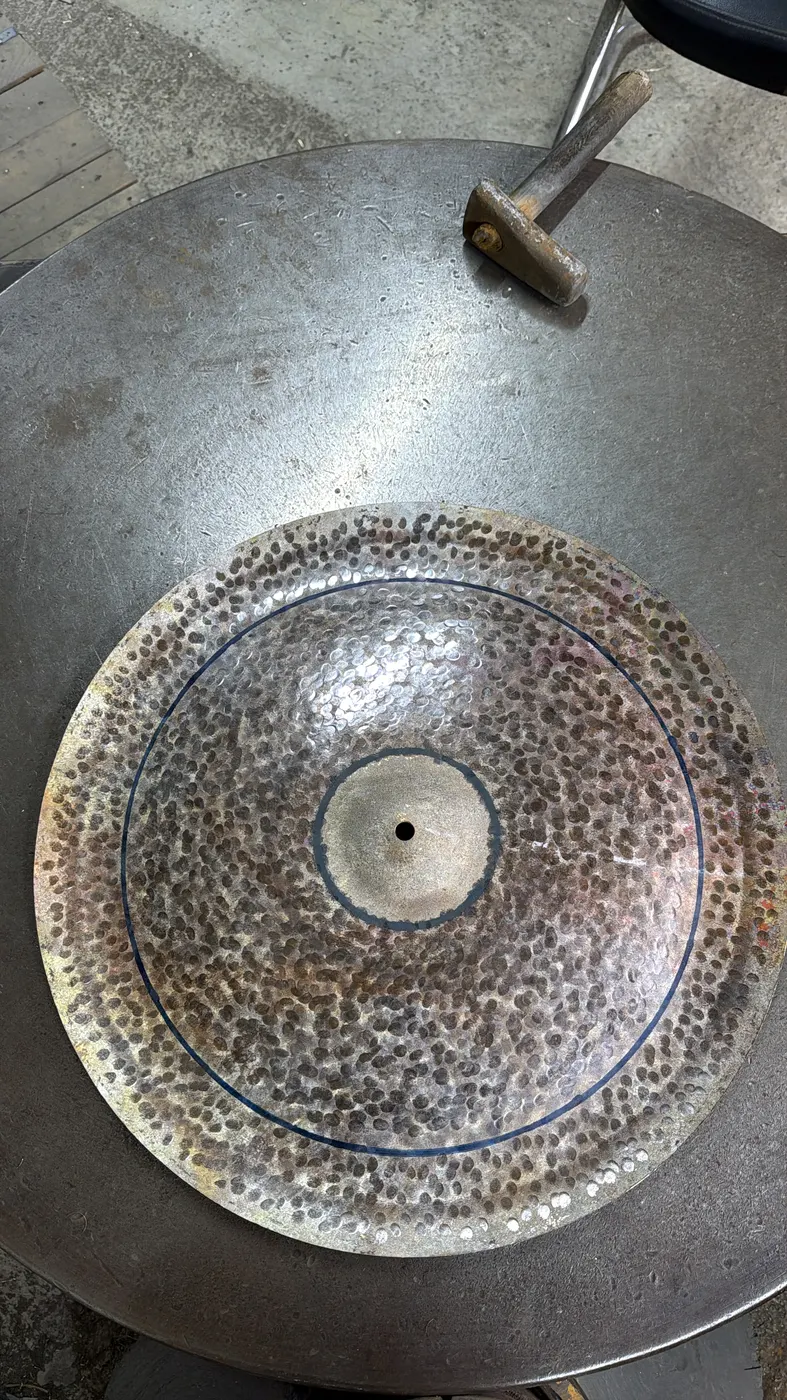
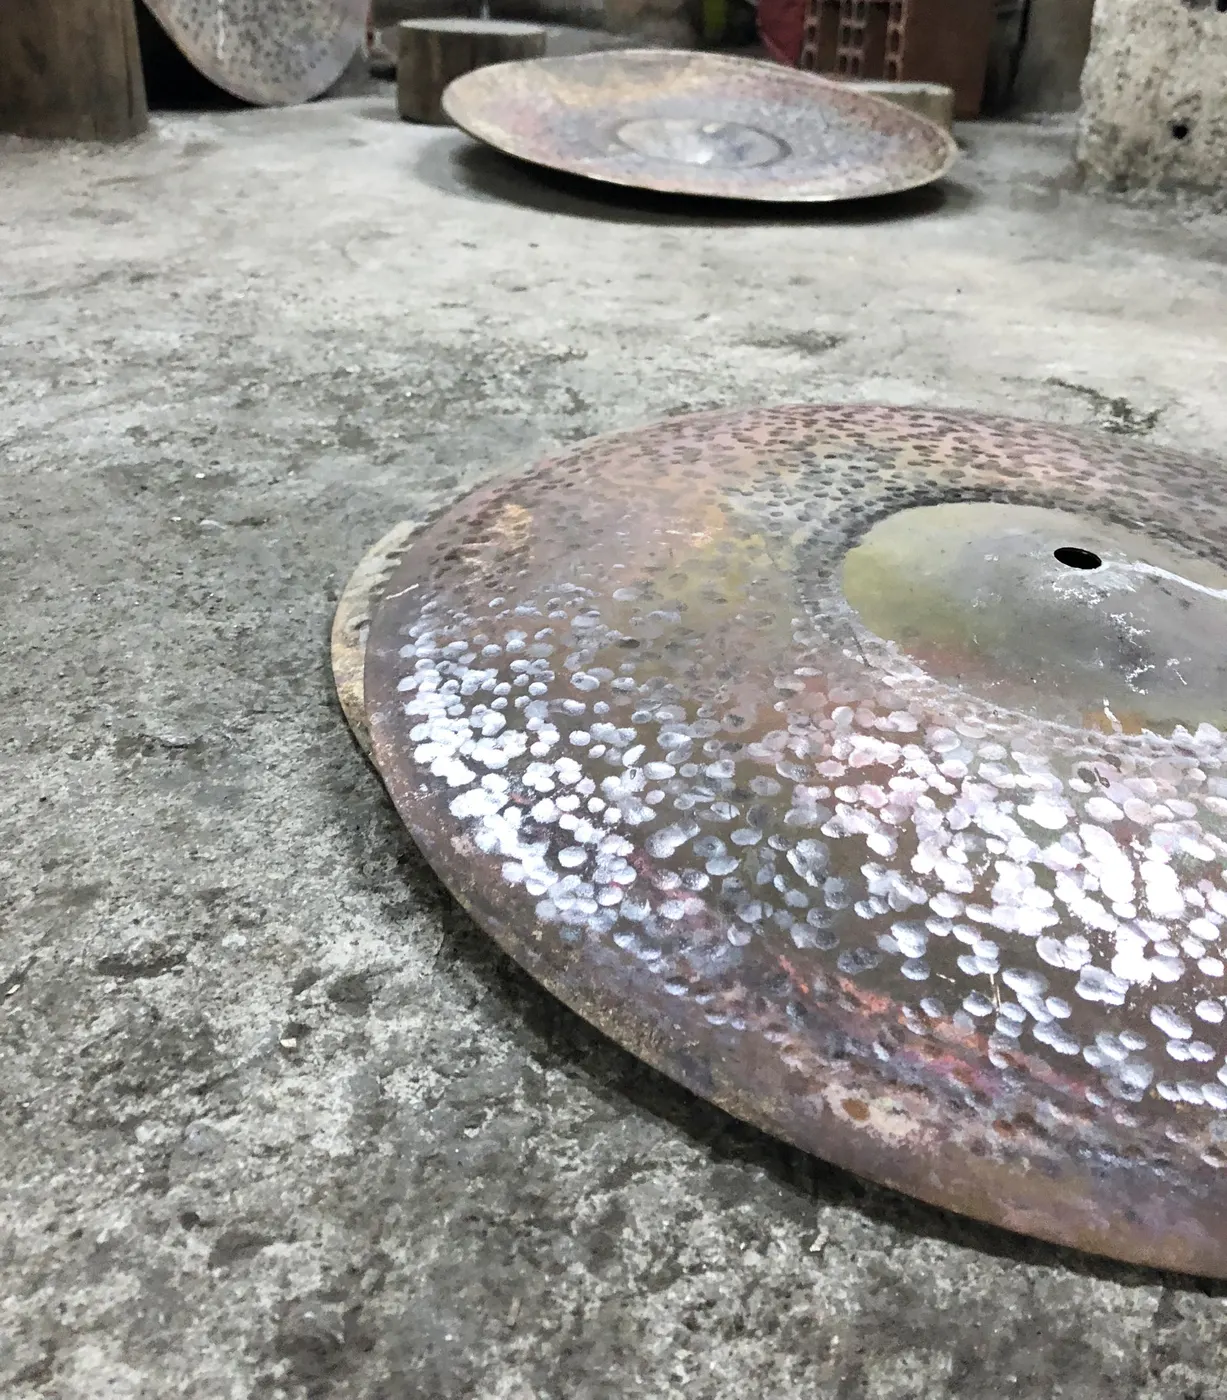
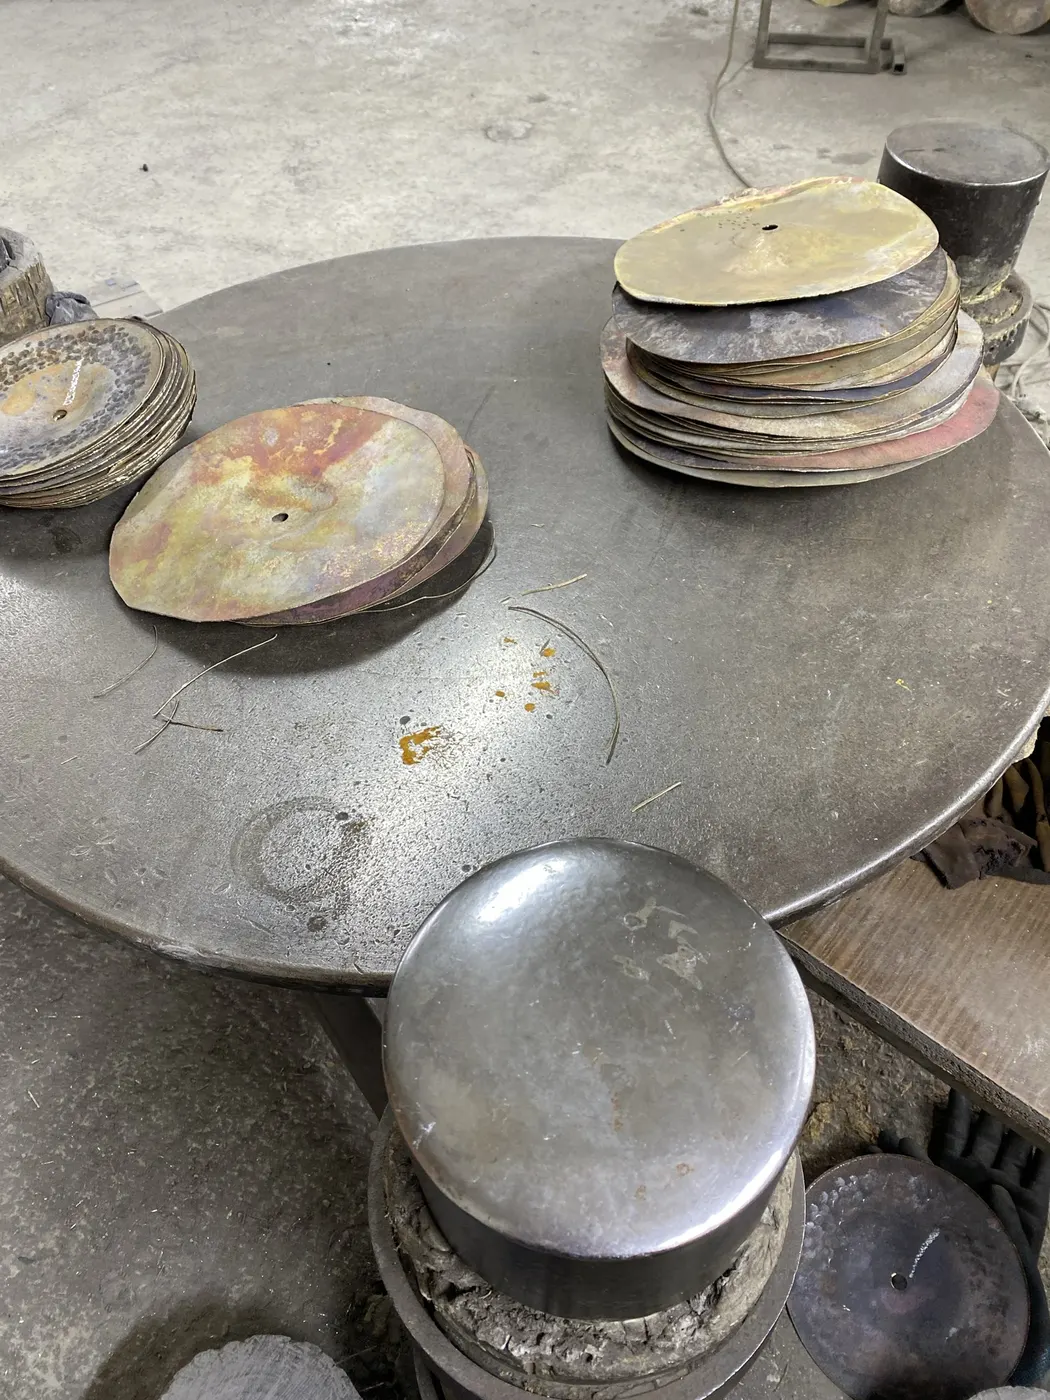


Samsun, Turkey
Keep scrolling. Night is falling.
Turkey’s largest cymbal production facility.
Every Diril is cast, rolled, hammered and lathed here, under one roof in Samsun.
How it’s made.
Seven steps from fire to sound. About three days and at least seven processes, all of it by hand.
Watch it on the home pageMelting
Copper melts at 1,085°C, tin at 232°C. Melted together, eighty parts copper to twenty parts tin, they become B20 bronze.
Casting
The molten bronze is poured into a small, thick disc. Around 15 cm wide and 5 cm thick, every cymbal starts here.
Rolling
Heated again and again, the disc is rolled out pass after pass until it reaches its size.
Tempering
A heat treatment in the oven gives the bronze its strength and its spring.
Creating the bell
The bell is formed at the centre. Its shape decides much of how the cymbal will speak.
Hammering
Thousands of strikes by hand. This is where a cymbal finds its character, and why no two are the same.
Lathing
Tonal grooves are cut on the lathe and the final weight is set. Then we listen, and only then does it leave the factory.